 Qingyuan moksha Biotechnology Co., Ltd

A sample that performs perfectly in a one-kilogram lab batch can behave differently in a two-tonne production vessel, and the difference is rarely caused by the formula. It is caused by the physics of the equipment: a different surface-to-volume ratio, a different shear profile, a different cooling rate. Scale-up is a process problem wearing the costume of a formulation problem. This guide covers what actually changes and how to manage it.
Why a Pilot Batch Is Not a Small Bulk Batch
In a small vessel, heating and cooling happen quickly because the distance heat has to travel is short. In a large vessel the same product may take many times longer to reach temperature and to cool afterwards, which changes the thermal history of every heat-sensitive material in the formula. The longer a sensitive material sits at elevated temperature in a large vessel, the more of it is lost.
Mixing behaves the same way. The element that produces motion at the vessel wall may leave the centre relatively still, and the relationship between impeller speed and actual shear in the product is not linear with volume. Matching impeller tip speed rather than revolutions per minute is the usual starting point for a scale-up calculation. Process capability is described in the workshop overview.
Mixing, Shear and Vessel Geometry
Emulsification depends on the energy delivered to the interface, so the homogeniser's power density, its position in the vessel and the batch volume all affect droplet size. A formula that reaches a target droplet size in two minutes at pilot scale may need a different pass count or a different homogeniser setting at bulk. Droplet size, not mixing time, is the parameter to hold constant across scales.
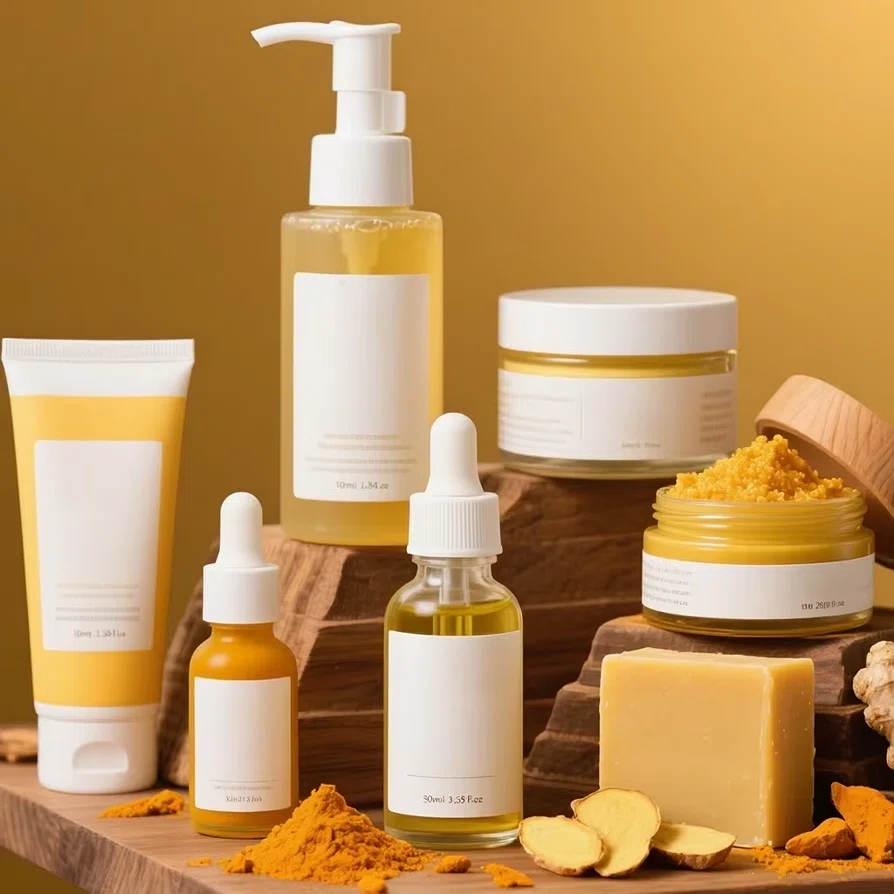
Vessel geometry adds another variable, because the ratio of height to diameter and the presence of baffles change flow patterns. A product that emulsifies cleanly in one vessel may aerate in another. Aeration is one of the most common scale-up defects, and it shows up as density variation or visible bubbles rather than as an obvious failure. One reference formulation direction in the current range is this light-texture cream base.
Powder addition and dispersion
Dispersing powders into a large volume is materially harder than in a beaker. Poor dispersion produces lumps that pass through the mill but reappear as grit, so the addition rate and the point of addition both belong in the batch record.
Temperature Control and Addition Sequence
With a longer heating and cooling cycle, the sequence of additions matters more. Materials that tolerate a short exposure to heat may not tolerate a long one, so a late-stage addition at pilot scale may need to become an even later one at bulk. Define a maximum hold time at temperature, and regard it as a hard limit rather than a target.
Cooling rate also affects crystallisation in systems that contain fatty alcohols or waxes. Slow cooling can produce a different crystal habit, which changes both viscosity and feel. Where a formula depends on crystallisation, the cooling profile is part of the specification and should be controlled, not left to the ambient temperature of the room.
Validation and First Three Bulk Batches
The first bulk batches should be treated as validation rather than as ordinary production. Sampling at defined points during the batch, plus full testing of the finished bulk, establishes whether the process is reproducible. Three consecutive batches meeting specification is a reasonable bar before a process is considered routine.
The comparisons worth making are not only pass or fail. Viscosity, pH, droplet size and appearance should be tracked against the pilot batch to see how far the process has drifted, because a result that sits inside the limit but at the edge of the expected range is a warning. Trending within specification catches problems that a pass or fail judgement hides until a batch genuinely fails.
Documentation and Change Control
The master batch record should carry the parameters that scale-up established: impeller speed and tip speed, homogeniser pass count, temperature set points with hold times, addition sequence and cooling profile. A parameter that only lives in an operator's memory is not a process, it is a dependency.
Change control then protects those parameters. A new homogeniser, a different vessel or a reformulated raw material all invalidate part of the scale-up work, and the notification requirement should cover them. Recording which vessel and which equipment were used for each batch is the cheapest way to explain a later deviation. Manufacturer credentials are summarised on the about us page, and project requirements can be submitted through the contact page.
Scale-up is where a good formula either becomes a reliable product or becomes a recurring production problem. Match tip speed rather than time, control the thermal profile, trend results instead of judging pass or fail, and write every parameter down. Send your project details through the inquiry form to plan a validation run.
Frequently asked questions
Can you produce Scale-Up from Pilot Batch to Bulk Production in Cosmetic OEM under our own brand?
Scale-Up from Pilot Batch to Bulk Production in Cosmetic OEM is handled as a private label project: you bring the brand and the market position, we cover formula, bulk, filling and packing. Existing bases can be adjusted for texture, fragrance and active level, or we develop from a new brief. Tooling and artwork belong to you, and our name does not appear on the pack.
What is the minimum order quantity?
MOQ is set by net fill per unit, not by category:
| Net fill | MOQ |
|---|---|
| < 15 ml/g | 5,000 pcs |
| 15-50 ml/g (50 included) | 3,000 pcs |
| 50-200 ml/g (200 included) | 2,000 pcs |
| > 200 ml/g | 1,000 pcs |
Several SKUs in one project can share a production run to reach the threshold, and a smaller trial order is possible once the formula is approved.
How long do samples and bulk production take?
Samples take 7-10 working days from a confirmed brief, or 10-15 days when a new mould or artwork is involved. Bulk runs 25-35 days after sample approval and packaging arrival. Repeat orders with an unchanged formula usually move faster.
Which certificates and documents come with the shipment?
The plant runs under GMPC and ISO 22716 with a 100,000-class cleanroom. Each shipment can include COA, MSDS, the full INCI list, stability data and microbiological reports. For the EU we support CPSR and PIF paperwork; for other markets we prepare the file set your importer asks for.
Can we change the formula, fragrance or packaging?
Yes. Texture, viscosity, fragrance, colour and active percentage are adjustable within regulatory limits. Packaging can be sourced by you or by us: tubes, airless bottles, jars, sachets and aluminium foil bags, with silkscreen, hot stamping or label application.
What information do you need to quote?
Category and target function, quantity per SKU, packaging direction, destination market and launch date. With that we reply within 24 hours on business days with feasibility, MOQ and a price range. An NDA can be signed before formulas are discussed.
Need this produced? Talk to the factory.
Wangsha Bio has run OEM/ODM production since 2006: 60,000 sqm plant, 17 lines, 100,000-class cleanroom, GMPC and ISO 22716 certified. Send your brief and we reply within 24 hours on business days with feasibility, MOQ and a price range.
Email lucky@moksha-bio.com | Product range | Workshop